Why Use a Food Inspection Metal Detector?
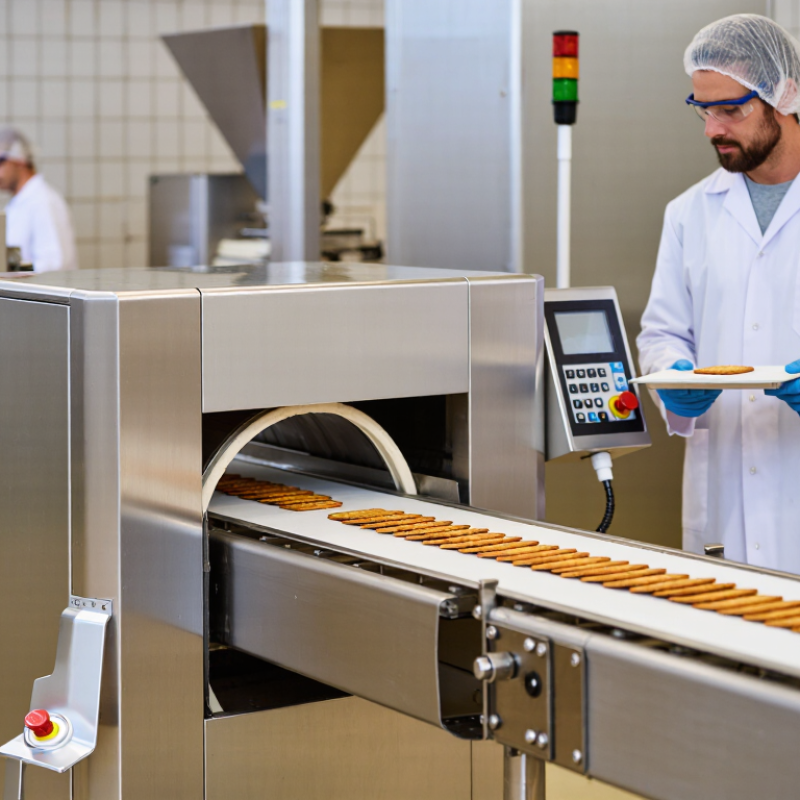
A Food Inspection Metal Detector helps manufacturers identify unwanted metal fragments before products reach consumers. It works quietly beside conveyors, checkweighers, and packaging lines. A passing biscuit may contain only grams of material, yet one small fragment can damage trust. Detection provides an important control point for products containing meat, bakery ingredients, dairy, snacks, and prepared meals.
Food safety consultant Dr. Richard Stier has expressed the practical principle clearly: “Metal detection is only one part of a broader food-safety system.” That statement matters. A detector cannot replace supplier approval, hygienic design, staff training, or careful process control. Instead, it supports a documented hazard-control program. In daily operation, technicians test calibrated samples, confirm reject timing, and examine alarms recorded during production. Ferrous, non-ferrous, and stainless-steel contaminants may require different sensitivity settings. Product moisture, salt, temperature, and packaging can also influence performance.
No detector is perfect. That deserves honest attention. A poorly positioned sensor may miss contamination, while excessive sensitivity may create repeated false rejects. Operators therefore need practical validation, stable installation, and clear response procedures. They should inspect the rejected product, isolate the affected batch when appropriate, and investigate the likely source. A loose mixer bolt, worn screen, or damaged blade can leave visible clues. The best reason to use a Food Inspection Metal Detector is not fear. It is disciplined prevention, supported by evidence, experience, and continuous review. Even a strong system needs questioning. That is where reliability begins.
What Is a Food Inspection Metal Detector? Three Contaminant Classes
Why Use a Food Inspection Metal Detector?
A food inspection metal detector checks packaged products for hidden metal fragments. It supports hazard control when visual checks cannot reveal small contamination. In production areas, fragments may come from worn blades, broken screens, or damaged conveyor parts. However, detection performance depends on product moisture, temperature, packaging, and detector settings. It is useful, but it is not a complete safety system.
Three contaminant classes usually matter: ferrous, non-ferrous, and stainless steel. Ferrous metals include iron and mild steel, which are often easiest to detect. Non-ferrous metals include aluminum, copper, and brass. Stainless steel can be more difficult, especially in wet or salty foods. This “product effect” can weaken the signal and create missed detections or false rejects. Operators should test sensitivity with approved samples at scheduled points. Records should include test time, product type, belt speed, and corrective action. Small details matter.
Tips: Place test pieces inside or beside the product, depending on your validated procedure. Check the smallest realistic package, not only an empty pouch. Keep the sensor opening clean and free from vibration. If rejection rates suddenly rise, stop and investigate before adjusting sensitivity. A stronger setting is not always better; it may increase waste without improving control. We have found that routine challenge testing exposes weaknesses early. Still, no detector replaces careful maintenance, supplier controls, and trained staff.
Why Use a Food Inspection Metal Detector?
Food inspection metal detectors help identify metallic contamination before products reach consumers. The three common contaminant classes are ferrous metals, non-ferrous metals, and stainless steel.
The chart compares the density of representative metals used to describe each contaminant class: iron for ferrous metal, aluminum for non-ferrous metal, and 304 stainless steel for stainless metal. Density is a physical reference only; actual detection performance also depends on particle size, product effect, orientation, moisture, and detector settings.
Where Metal Contamination Enters: HACCP Hazard Analysis and CCP Control
Why Use a Food Inspection Metal Detector?
Metal contamination can enter food during harvesting, processing, maintenance, or packaging. A broken blade, loose screw, or worn conveyor part may fall into a product without obvious warning. The risk is practical, not theoretical. The World Health Organization estimates that 600 million people become ill from contaminated food each year, with 420,000 deaths reported globally (WHO, 2015).
HACCP hazard analysis should identify where metal can enter, how likely it is, and how serious the outcome could be. Codex Alimentarius states that critical control points require measurable control and verification (CXC 1-1969, 2022 revision). In many production lines, a metal detector becomes a CCP after sealing or before dispatch. Operators should test it with certified ferrous, non-ferrous, and stainless-steel test pieces. They should also record rejection performance, product settings, and corrective actions.
Small details matter. Wet products, salt, foil packaging, and temperature changes can create product effects that reduce detection stability. A detector can also reject safe products if sensitivity is set carelessly. That wastes food and hides the real problem. Not perfect. Validation should challenge the system at the fastest line speed and the weakest detection position, usually near the center of the product aperture. The FDA’s preventive controls framework requires facilities to monitor hazards and verify that controls work as intended (FDA, 2015). Without documented checks, a metal detector is only equipment, not effective HACCP control.
How Detection Works: Electromagnetic Fields, Product Effect, and Sensitivity
A food inspection metal detector creates an electromagnetic field inside its aperture. Three coils usually perform the work: one transmitter and two receivers. When metal enters the field, it changes the signal balance. The system then triggers a rejection response.
The science becomes harder with real food. Moist, salty, or warm products conduct electricity and create “product effect.” This signal can resemble a small metal fragment. The detector must separate food behavior from contamination. Product trials should measure ferrous, non-ferrous, and stainless-steel test pieces at the weakest detection point. Usually, that point is near the aperture center.
Small details matter. A larger opening often reduces sensitivity. Faster conveyor speeds can shorten detection time. Product orientation also changes results. A thin wire may pass differently from a compact sphere. Temperature drift, vibration, and poor calibration can create false confidence. The FDA Food Code 2022 identifies physical hazards as a food safety concern, while the WHO’s 2015 global burden report estimated 600 million foodborne illnesses and 420,000 deaths annually. Metal detection cannot address every hazard, but it provides a measurable control for metallic contamination.
It is not perfect.
Operators should record challenge-test results, product temperature, line speed, and rejection performance. Reviewing these records can expose weak settings. In practice, the best sensitivity is not the lowest displayed number. It is the lowest reliable result achieved under actual production conditions.
